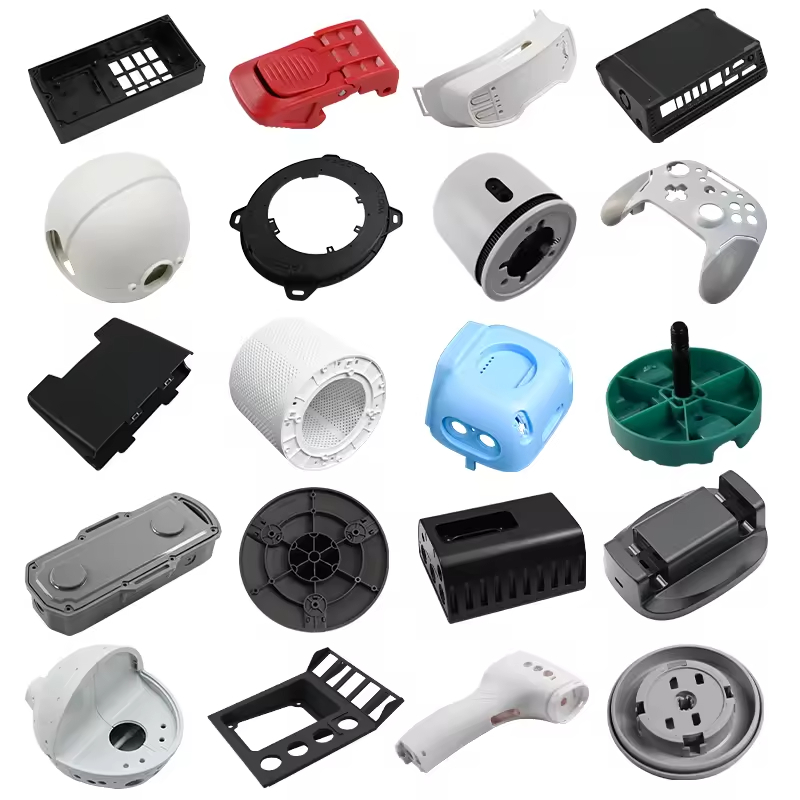
Low-volume injection molding makes limited batches of plastic parts using a qualified mold and a defined resin grade. It can support pilot production, end-use small batches, bridge supply and replacement parts when the design and demand justify tooling.
Choose the Route Around the Part
Quantity alone does not select the process. Review design stability, required material, critical dimensions, test purpose, repeat demand and tooling investment. A printed or machined sample may answer an early design question; a molded sample may be needed to validate molded behavior.
Send CAD, the drawing, material requirements and batch forecast. Nylon Plastic can compare prototype, CNC and molding routes and define the tooling, sample and production scope for quotation.
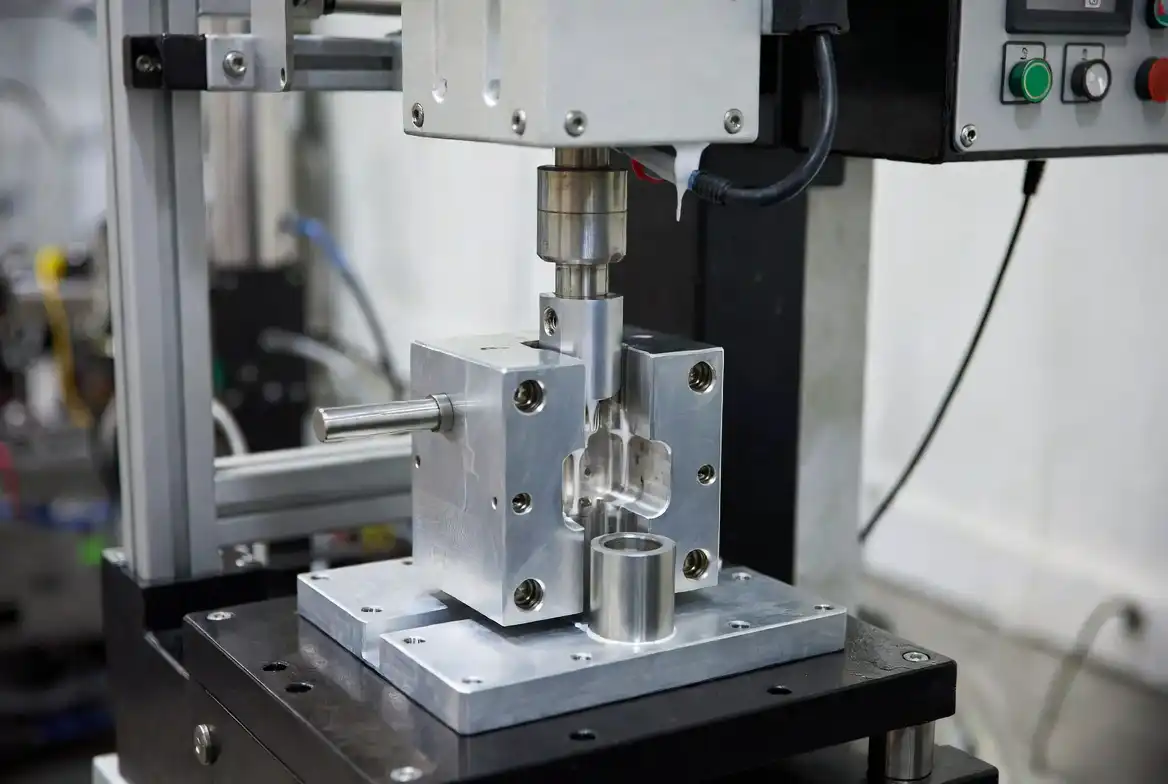
Low-Volume Injection Molding vs 3D Printing and CNC
Start with the evidence the parts must provide. Visual review, assembly fit, mechanical testing and production approval can require different materials and processes. There is no universal quantity at which every project should switch to a mold.

| Маршрут | Useful project task | Decision limit |
|---|---|---|
| 3D-печать | Early geometry, fit or a suitable additive end-use application | Check layer behavior, finish and whether the printed material meets the test requirement |
| Обработка на станках с ЧПУ | Functional samples or limited batches from available engineering plastic stock | Check tool access, stock grade, conditioning and recurring machining cost |
| Low-volume injection molding | Pilot or limited production requiring a molded material and process | Needs tooling review, a controlled design and trial approval |
| Production injection molding | Stable repeat demand where a production tool is justified | Higher investment must be assessed against output, wear and accepted-part cost |
When comparing routes, include the whole program: sample iterations, material availability, post-processing, inspection, repeat orders and changes to the drawing. An inexpensive early sample can still be the wrong evidence for final-part approval. Our plastic prototype manufacturing guide covers the earlier development stage.
Select Tooling for the Resin and Program
Low-volume tooling does not mean a particular mold metal, guaranteed mold life or reduced inspection. Resin reinforcement, processing conditions, geometry, finish, maintenance and expected demand all affect the tool specification.

| Tool option | Reason to review it | Requirement to confirm |
|---|---|---|
| Aluminum mold | A potential route for a limited program where resin and features permit | Wear, finish, cooling, maintenance and achievable acceptance |
| Pre-hardened steel mold or inserts | A potential choice where resin wear, finish or repeat demand favors steel | Steel selection, critical surfaces, repair strategy and trial scope |
| Replaceable mold inserts / shared frame | Can separate a reusable frame from part-specific cavity work | Frame compatibility, ownership, part envelope and future transfer |
| Production-oriented tooling | May suit sustained demand or a demanding process despite a small first order | Cavity strategy, output, qualification, maintenance and program economics |
For glass-filled engineering plastics, review wear-prone gates, shutoffs and cavity surfaces alongside the required finish and dimensions. Confirm the intended tool service life, repair approach and inspection intervals in the quotation rather than relying on a generic shot-count range.
Compare Total Program Cost, Not Only Part Price
Separate mold investment from recurring production cost. A lower tool price may involve a different cavity count, loading method, runner system, sample package or maintenance assumption. Compare the same grade, drawing revision, quantities and delivered scope.
| Cost area | Questions for a comparable quote |
|---|---|
| Инструментальная оснастка | Which cavities, actions, runner, steel or aluminum, texture and trial corrections are included? |
| Parts | Which resin grade, color, regrind policy, inserts, finish and order quantities are quoted? |
| Qualification | Which samples, dimensional records and functional tests are included or excluded? |
| Повторная поставка | What setup, maintenance, storage, spare inserts or material minimums affect later orders? |
| Доставка | Which packaging, destination, delivery terms and shipment assumptions apply? |
A simplified break-even calculation is additional tooling investment ÷ recurring saving per accepted part. Use it only when the saving is positive and both quotations cover equivalent parts. Add qualification, maintenance, resin waste, changes, freight and inventory before making the sourcing decision. The Руководство по стоимости литья под давлением develops that comparison.
Plan Samples and Delivery Milestones
Request a schedule tied to released inputs: drawing approval, resin availability, tool design approval, trial samples, corrections, sample acceptance and production. A tool-completion date is not necessarily a date for approved finished parts.
- Agree the baseline: CAD revision, grade, color, critical dimensions, finish and quantities.
- Review DFM: draft, walls, undercuts, gates, ejection, inserts and shrinkage assumptions.
- Define trial acceptance: sample quantity, dimensional report, visual reference and functional tests.
- Release the batch: confirm approved samples, inspection, packaging and delivery conditions.
For nylon components, specify the conditioning state used for inspection and testing. Where regulatory or customer documentation is required, confirm its applicability to the exact grade and production scope. Low demand does not remove those requirements.
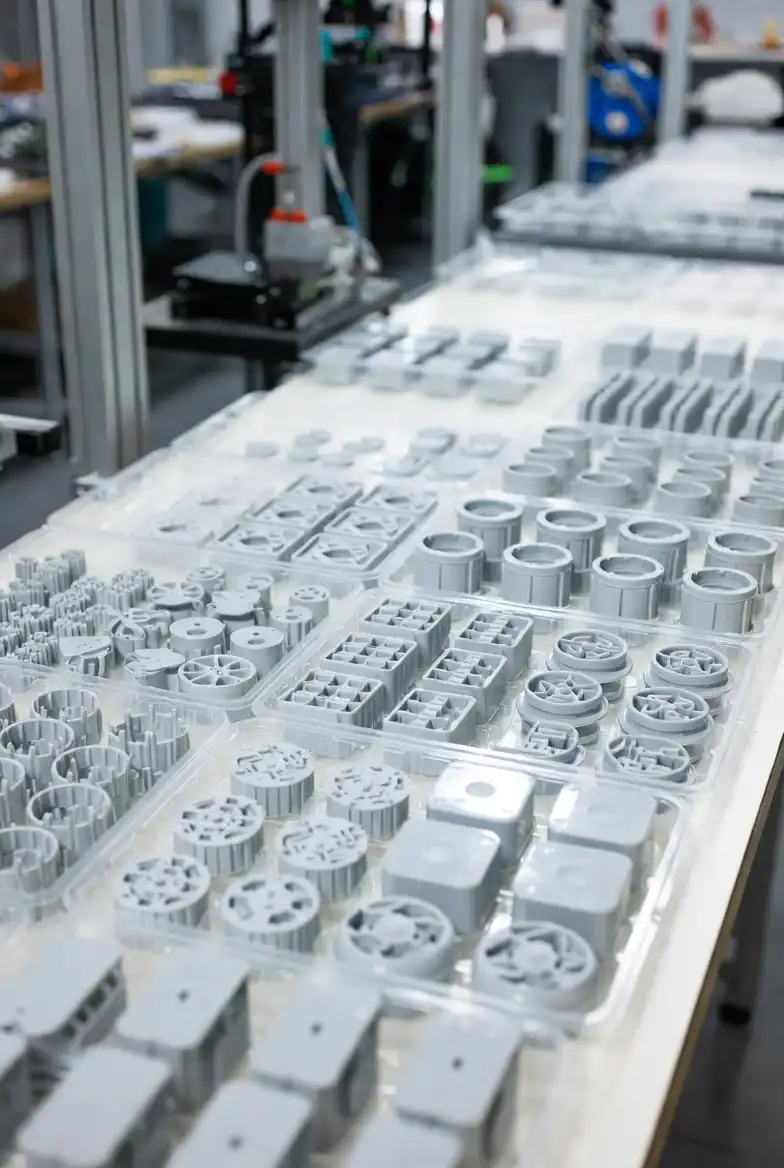
Bridge Production and the Move to a Production Tool
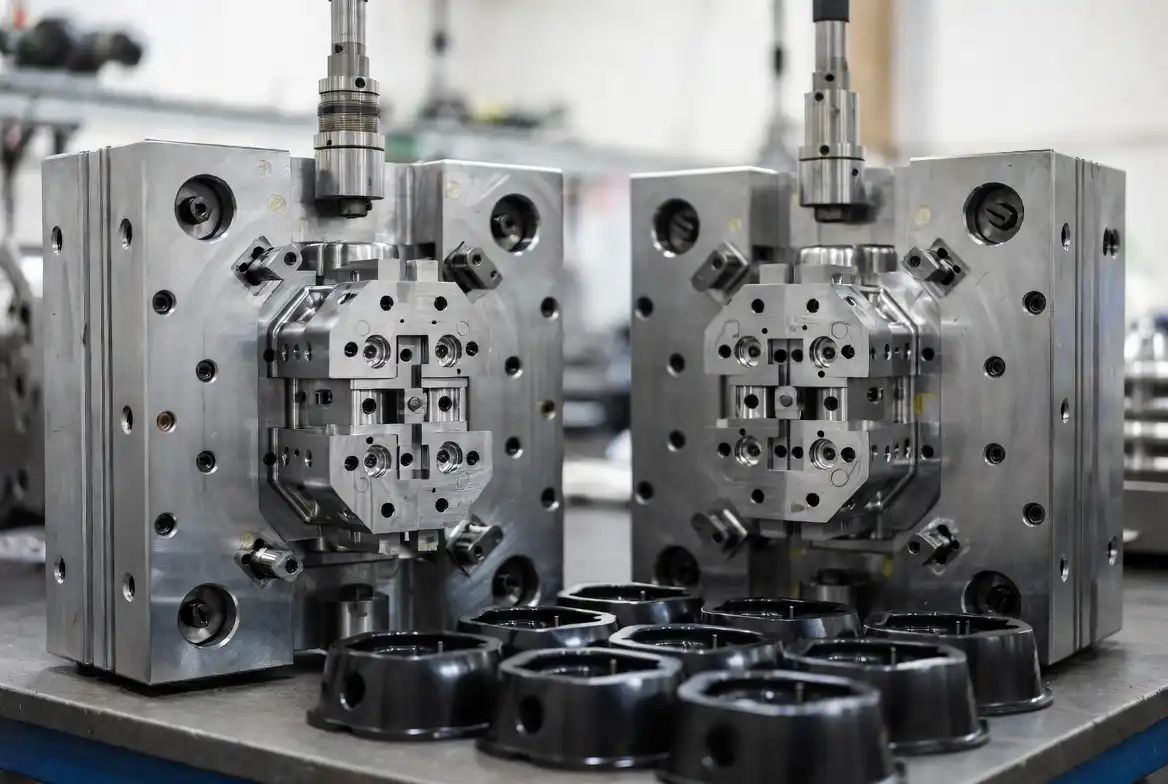
A bridge mold can supply approved parts while a later production route is prepared. The handover needs its own qualification; do not assume a new mold will reproduce every dimension, appearance or interface without trials.
- Demand: review released orders, credible forecasts, peak output and the remaining program life.
- Состояние инструмента: track wear, flash, dimensional drift, maintenance and repair needs.
- Process economics: compare cavities, cycle, loading, inspection and recurring accepted-part cost.
- Transfer record: carry forward the approved drawing, resin, samples, process records, defect history and acceptance criteria.
Обзор rapid versus production tooling before deciding whether to retain, modify or replace the bridge tool.
Пример из практики: Корпус автомобильного датчика
Один из поставщиков автомобильной промышленности первого уровня (Tier 1) нуждался в 8 000 корпусов датчиков, изготовленных методом литья под давлением из PA66, армированного стекловолокном, для программы валидации предсерийного автомобиля. Стоимость полного производственного инструмента — пресс-формы из закаленной стали S136 с системой горячеканального литья — была оценена в $85 000 со сроком изготовления 14 недель. В рамках промежуточной стратегии была использована алюминиевая форма по цене $12 000 со сроком изготовления 4 недели, что позволило изготовить всю необходимую партию из 8 000 единиц за 10 дней литья. Общая стоимость, включая изготовление пресс-формы и производство, составила примерно $38 000. Альтернативный вариант — отсрочка программы на 10 недель и переход непосредственно к изготовлению серийного инструмента — повлек бы за собой штрафы за задержку программы на сумму, превышающую $100 000, и поставил бы под угрозу отношения с поставщиком. Переходная форма успешно обеспечила выпуск всех необходимых деталей в соответствии с техническими требованиями и была оставлена для производства запасных частей.
RFQ Checklist for Low-Volume Molded Parts
| Send this information | Why it changes the review |
|---|---|
| CAD and controlled drawing | Defines geometry, revision, datums, tolerances, inserts and cosmetic surfaces |
| Exact grade or service conditions | Sets material choice, reinforcement, conditioning and applicable documentation |
| First batch and repeat forecast | Supports route, cavity, stock and tooling-investment decisions |
| Approval requirements | Defines samples, critical dimensions, appearance, tests and records |
| Tool expectations | Clarifies ownership, maintenance, storage, life requirement and transfer terms |
| Delivered scope and timing | Defines secondary operations, assembly, packaging, destination and milestones |
Supporting design decisions include gate selection, tool steel selection и tolerance stack-up. Mark mandatory requirements and identify where an alternative is acceptable.
Request a Low-Volume Injection Molding Review
Nylon Plastic connects engineering material selection and supply with prototyping, CNC machining, mold review and injection molding. The review can identify route and tooling questions and the sample evidence needed before production.
Tool ownership, maintenance, documents, delivery timing and the included manufacturing scope are confirmed for your specific quotation.
Часто задаваемые вопросы
Каков минимальный объём заказа при мелкосерийном литье под давлением?
There is no universal minimum. Part geometry, resin availability, setup, tooling and the approval requirement affect the practical batch size. Send your first-order and repeat quantities for a project-specific review.
Is aluminum always the best low-volume mold material?
No. Resin reinforcement, wear, temperature, geometry, finish and expected repeat demand can favor another tool material. Confirm the tool specification and service-life requirement for the project.
Can I validate the molded part with a 3D-printed sample?
A print can answer some geometry or fit questions. It does not automatically validate the molded grade, fiber orientation, weld lines, shrinkage or final production process. Define which tests require molded samples.
Can low-volume parts have controlled finishes and inspection reports?
They can be specified as part of the project scope. Send the finish reference, critical dimensions and required records; applicability and included work should be confirmed in the quotation.
How do I move from bridge molding to production?
Transfer the approved drawing, grade, samples and process records, then qualify the production tool against the agreed requirements before switching supply.
Сопутствующие технические руководства
- Руководство по расчету затрат на литье под давлением
- Planning Injection Molding Lead Time
- Руководство по замене металла на пластик
For broader DFM, material, tooling and production support, review our услуги по литью пластмасс под давлением and send the part drawing, material requirements and expected quantity with the RFQ.